How Do I Check a Panel OEM Supplier's Production Capacity?
How Do I Check a Panel OEM Supplier's Production Capacity?
How do I check a panel OEM supplier's production capacity? Start by looking beyond the supplier’s stated monthly output. For decorative panel buyers, reliable capacity depends on production lines, material availability, order complexity, quality controls, and delivery performance. A factory may have impressive equipment yet struggle to meet your specifications or peak-season deadlines. This guide explains how to assess production records, verify capacity during a factory visit, and ask the right questions before placing an OEM order.
The question is not simply whether a factory can make panels. It is whether it can make your panels, in the required quantity, at the required quality, within a production slot that is available to you. Those conditions should guide every document request, site visit, and commercial discussion.
Turn a monthly capacity claim into a usable number
A supplier may quote capacity in square meters, sheets, containers, or production lines. None of those figures is useful until you know what it includes. Ask which panel construction, sheet dimensions, thickness, finish, shift pattern, and product mix were used to calculate the number. Also ask whether it represents theoretical output, actual historical output, or capacity currently available for new orders.
The distinction matters. A line producing a standard flat panel continuously may achieve a different output from the same line running several custom colors, protective films, or cut-to-size orders. Changeovers take time, and some orders need additional inspection or packaging. If the supplier’s figure assumes uninterrupted production of one simple product, it should not be treated as a delivery commitment for a mixed OEM program.
A practical calculation begins with the capacity of the limiting process, not the fastest machine:
Estimated good output = available production time × output rate at the bottleneck × expected proportion of acceptable panels.
Use actual operating records where possible. Available time should account for maintenance, changeovers, planned stoppages, and existing bookings. The acceptable proportion should reflect the relevant specification and inspection criteria, not an assumed perfect yield. This estimate is a planning tool, not proof that a slot has been reserved.
Trace your order through the bottleneck
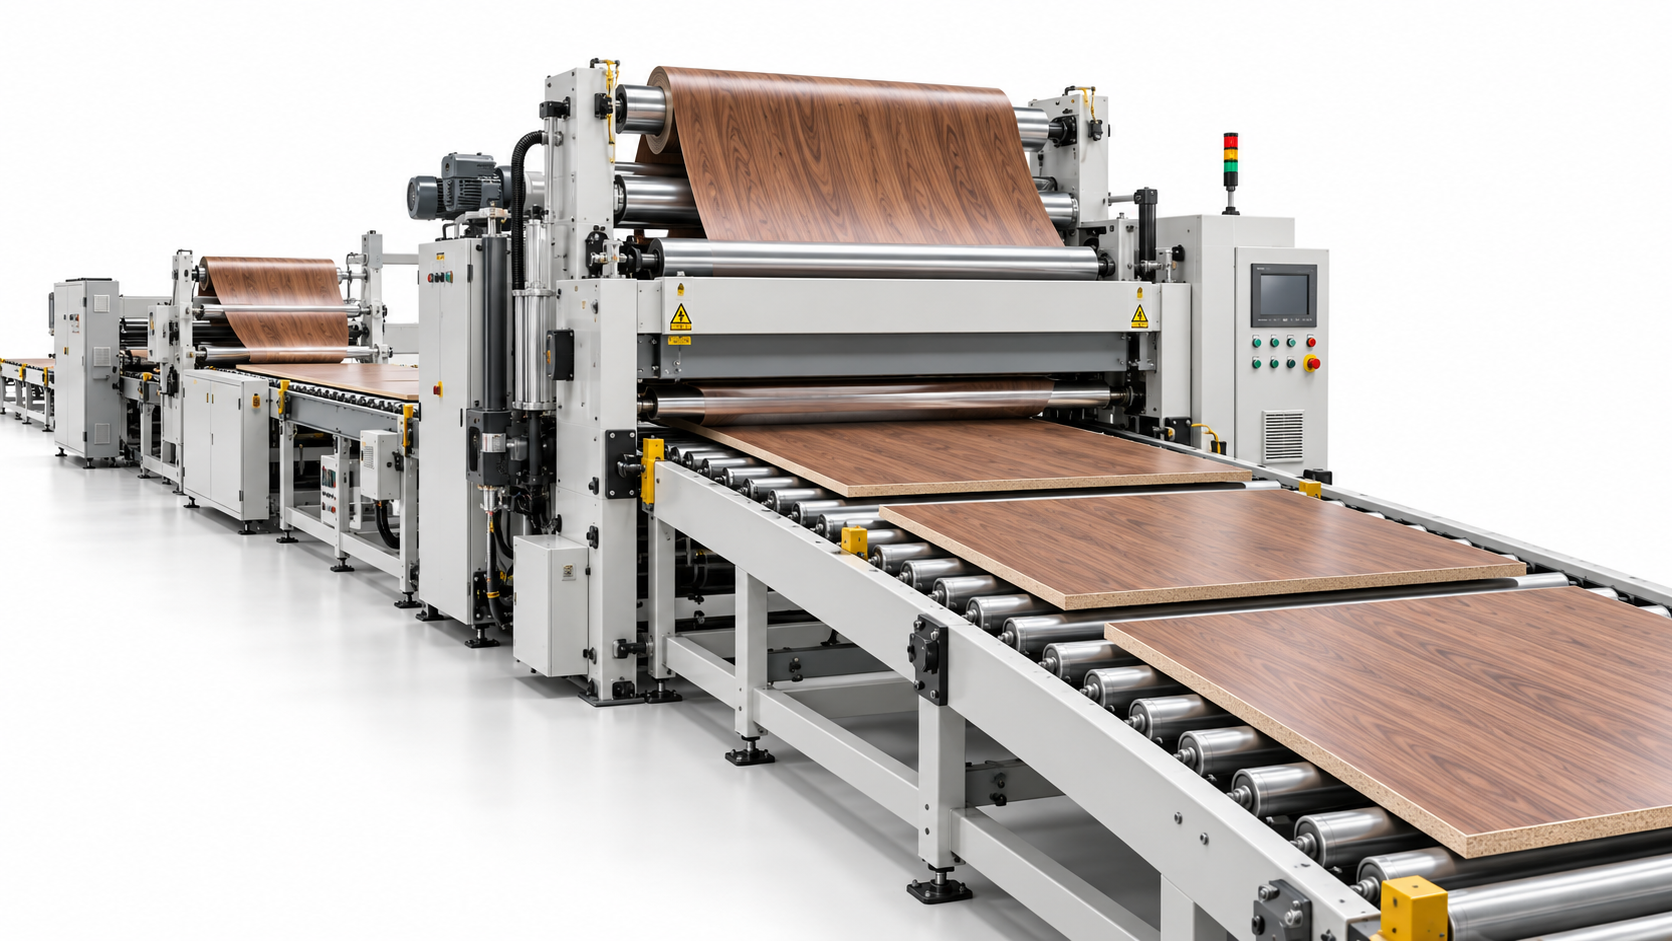
Decorative panels can involve several operations: substrate preparation, surface application, pressing or curing, trimming, inspection, and packing. The exact sequence depends on the material and finish. A supplier may own a high-speed cutting line but rely on a slower press, a limited curing area, or manual finishing. The slowest constrained step determines how much finished product can leave the factory.
Ask the production manager to map your proposed order from incoming materials to packed goods. Where are panels likely to wait? Which operations are shared with other customers? Can different colors or surface textures run together, or do they require cleaning and setup between batches? A credible answer identifies constraints and explains how the schedule accommodates them. An answer that relies only on the number of machines leaves too much unanswered.
Pay particular attention to outsourced steps. Printing, coating, lamination, special cutting, or packaging may be performed by another company. Outsourcing is not automatically a weakness, but the quoted capacity should reflect the subcontractor’s availability as well as the panel factory’s own schedule. Ask who controls quality at the handoff and what happens if the external process is delayed.
Request evidence that connects output to delivery
A useful document review follows the flow of a real order. Subject to confidentiality, ask for anonymized records covering a comparable product and production period. One document on its own rarely tells the whole story; the value is in checking whether the quantities and dates agree across records.
- Production plans and daily output records: Check planned versus completed quantities, product type, shifts, downtime, and rescheduled work.
- Quality and rework records: Look for rejected quantities, recurring defects, and whether reworked panels were included in reported output.
- Material purchasing and inventory records: Confirm whether key substrates, decorative films, coatings, adhesives, and packaging were available when needed.
- Dispatch records: Compare finished quantities and dispatch dates with the agreed production schedule. Where appropriate, separate factory delays from carrier or buyer-side delays.
- Maintenance and staffing plans: Check whether the production window depends on extra shifts, specialist operators, or equipment due for maintenance.
Confidentiality may prevent a supplier from sharing customer names or commercial terms. Redacted records can still show dates, quantities, and process stages. If the factory cannot provide any consistent evidence, treat the capacity figure as unverified rather than assuming it is false—or accepting it at face value.
Use the factory visit to test the story
A visit is most useful when it takes place during normal production. Before arriving, share the panel specification and ask to see the processes that would actually handle your order. A clean showroom and a row of idle machines do not establish production capacity.
Follow material through the plant. Check whether work-in-progress is identified by batch, whether operators can explain the current job, and whether finished panels are protected from scratches, contamination, and edge damage. Ask how the factory handles color variation and surface defects, especially when a project requires panels from several batches to be installed together.
The condition of the warehouse is also relevant. Substrates and finishes may need controlled storage or handling appropriate to the material. Poor stock identification can cause the wrong film, thickness, or finish to enter a production run even when the machines are capable of the work. Observe how accepted, rejected, and uninspected goods are separated.
If an on-site visit is impractical, a live video walkthrough can help, particularly when the supplier shows production records alongside the operating line. It is still a limited substitute: camera angles, timing, and access may restrict what you can verify. An independent audit or inspection may be worthwhile when order value, technical risk, or delivery exposure justifies it.
Check material supply as carefully as machine output
The factory’s nominal output is irrelevant if the specified surface film or substrate cannot arrive on time. For each critical material, ask whether it is stocked, ordered after deposit, or sourced against a separate lead time. Confirm minimum purchase quantities, alternatives, and the approval process for substitutions.
This is especially important for private-label finishes. A custom pattern may require artwork approval and a separate production run before the panel line can start. Color matching, protective film, labels, and cartons can also become schedule dependencies. A supplier should be able to distinguish material lead time from manufacturing time rather than presenting one optimistic number.
For construction and furnishing applications, documentation needs may affect the schedule too. If the project requires evidence of fire performance, emissions, or other properties, confirm the applicable local requirements and whether the evidence covers the actual panel construction. A report for a different substrate or finish should not automatically be assumed to apply. Allow time for review or testing where required.
Separate available capacity from a promise
A factory might have sufficient average output but no open slot when your project needs it. Ask for a dated production plan showing material arrival, sample approval, manufacturing, inspection, packing, and dispatch. Identify the event that starts the clock: an approved drawing, a confirmed color sample, receipt of payment, or arrival of a particular material.
For a staggered project, agree on shipment lots rather than relying only on a final completion date. Clarify whether the supplier can hold finished stock, how panels will be packed, and whether batches need to be shipped together for visual consistency. If demand may increase, ask what extra quantity could be accommodated and how much notice would be needed. Do not treat unused theoretical capacity as an automatic reservation.
It is also worth agreeing on escalation before an order is delayed. Who reports a material shortage or equipment failure? How often will the schedule be updated? Can a partial shipment be released without affecting color matching or installation sequence? These details are more useful than a general assurance that the supplier will “do its best.”
Use a trial order to verify both quality and repeatability
A sample shows what a supplier can make under controlled conditions; it does not necessarily show how a full run will perform. A trial order can reveal changeover losses, batch variation, packing problems, and the time required to resolve defects. Make the trial representative: use the intended substrate, finish, dimensions, tolerances, labeling, and packaging wherever practical.
Before production starts, approve a reference sample and define how acceptance will be judged. Depending on the application, that may include dimensions, flatness, surface appearance, color consistency, adhesion, and damage after handling. Specify inspection timing and who has authority to release or reject goods. If defects are found, agree on whether replacement, sorting, or rework is acceptable and how each option affects the delivery date.
One successful trial is useful evidence, but it does not establish unlimited capacity. Compare the trial schedule with the proposed full order: a larger volume may involve more material batches, longer runs, additional shifts, or subcontracted operations that were not tested initially.
Make the comparison specific to your project
When comparing suppliers, use the same specification and delivery assumptions for each quotation. A lower price based on standard sizes, limited inspection, or generic packaging is not directly comparable with an offer covering custom finishes and staged deliveries. Record the assumptions alongside the quoted capacity so that a later change in scope does not become a surprise.
Shenyang Shengshi Meilin Technology Co., Ltd., based in Shenyang, focuses on new material technology and offers products and services spanning materials, fireproof sealing materials, furniture, and home furnishings. For a buyer discussing a decorative-material project with the company, that breadth can be a useful starting point for a technical conversation. The specific panel process, available production slot, supporting documentation, and OEM scope should still be confirmed for the order in question.
A sound decision comes from matching a documented production plan to a clear specification. Before committing, confirm the bottleneck, material lead times, acceptance criteria, available slot, and dispatch arrangements in writing. If any of those remain assumptions, they belong on the risk list—not inside the supplier’s capacity figure.
RECOMMEND

Nov 03, 2026
How to Keep Wall Panel Color Consistent Across Batches and Repeat Orders
Color drift between batches is a process problem, not luck. The batch-control workflow buyers should write into the order before a repeat purchase.
Nov 03, 2026
Are Stone-Look Panels Cheaper to Install Than Natural Stone?
Are stone look panels cheaper to install than natural stone? Compare labor, materials, wall preparation, and hidden costs to choose the best option for your project.
Nov 03, 2026
How Do I Check a Panel OEM Supplier's Production Capacity?
How do I check a panel OEM supplier's production capacity? Learn to verify output, materials, quality and delivery before placing your decorative panel order.
Nov 02, 2026
Will a PUR-Laminated Panel Delaminate in a Humid Room?
Will a PUR laminated panel delaminate in a humid room? Discover what affects moisture resistance and how to choose the right panel for your bathroom or kitchen.